Buying guide · Rolling & Forming
Best Rolling Mills for Home Jewelers
Choose the right jewelry rolling mill by roller width, configuration, gearing and bench space, with a research-based look at budget and professional options.
Rolling & FormingExplainer
How to choose rolling mill size for jewelry making — usable flat width vs roller width, 80 vs 110 vs 130 mm mills, cuffs, texture plates and bench space.
For most jewelry makers, a rolling mill with about 100–130 mm (4–5 inches) of total roller width is the most flexible size range.
A smaller 75–80 mm mill can be enough if you mainly make rings, earrings, bezels, narrow pendants and wire. A 100–110 mm mill gives you more room for general bench work, while a 130 mm or wider mill becomes useful when you regularly work with wider sheet, cuffs, larger texture plates or production work.
But there is an important catch: do not choose a rolling mill from its advertised roller width alone.
On a combination mill, part of the roller may be occupied by square-wire and half-round grooves. A mill advertised as 110 mm wide might therefore have substantially less than 110 mm of smooth flat rolling surface.
Quick answer
For most jewelry makers, 100–130 mm of total roller width is the most flexible range. Before buying, check the total roller width, the usable flat rolling width, the maximum roller opening, the roller diameter, the gear reduction and the widest piece of metal you actually expect to roll. For most buyers, usable flat width is the measurement that matters most.
| Rolling mill size | Usually best for | Main limitation |
|---|---|---|
| 45–60 mm | Wire, ring stock, tiny components, very small benches | Quickly restrictive for sheet work |
| 75–80 mm | Rings, earrings, bezels, small pendants and occasional sheet | Limited room for wider sheet and texture plates |
| 90–110 mm | General jewelry making and small studio work | Combination mills may have a much narrower flat section |
| 120–130 mm | Wider sheet, bracelets, cuffs and frequent texture work | Larger, heavier and normally more expensive |
| 140–165 mm+ | Wide sheet and production-oriented work | Often unnecessary for a typical home jewelry bench |
These ranges are guides rather than strict rules. Two mills with the same nominal width can have very different usable capacities.
When manufacturers describe a mill as 80 mm, 110 mm or 130 mm, they are normally referring to the overall length of the working roll.
That does not necessarily tell you how wide a sheet of metal you can roll.
A flat mill dedicates most or all of its working roll to a smooth surface.
If your work consists mainly of:
a flat mill can give you considerably more useful sheet capacity for a given overall roller size.
A combination mill divides the roller between a smooth section and shaped grooves for wire.
That makes it more versatile, but there is a trade-off: the usable flat section can be considerably narrower than the advertised roll width.
For example, a 110 mm combination mill might devote only around half of the roll to flat sheet while using the remainder for square and half-round wire grooves.
That is why comparing a 110 mm flat mill with a 110 mm combination mill as though they have identical sheet capacity can be misleading.
If you expect to roll sheet frequently, always find the manufacturer’s specification for flat rolling area, not just total roller length. Our combination vs flat rolling mill comparison covers this trade-off in more detail.
For many first-time buyers, the decision eventually comes down to three approximate size classes.
An approximately 80 mm mill makes sense when bench space and budget matter more than maximum sheet capacity.
It can be suitable for:
For a jeweler who mostly works on small components, this may genuinely be all the mill required.
The disadvantage is not that an 80 mm mill produces worse jewelry. It is simply easier to outgrow.
A project that is slightly wider than your available flat section cannot be rolled evenly in one normal pass. Wider texture plates can also become inconvenient.
Choose around 80 mm if: your projects are consistently small, space is tight, or you are buying an inexpensive first mill to learn on.
Look wider if: bracelets, cuffs, wider sheet or larger textures are already part of your plans.
The 100–110 mm class is a useful compromise between capacity, bench footprint and cost.
It is suitable for much of the work encountered at a general jewelry bench:
For a home workshop where the rolling mill must fit alongside a soldering area, flex shaft, bench pin and other equipment, this size can make more sense than automatically buying the largest machine available.
Again, check the roller configuration. A 110 mm flat mill and 110 mm combination mill can provide very different amounts of smooth rolling surface.
Choose around 100–110 mm if: you want one versatile mill for normal jewelry-scale projects and do not routinely work with wide sheet.
A 130 mm-class rolling mill gives you more flexibility before project width becomes a constraint.
That extra capacity can matter for:
The mill will normally be heavier, require more bench space and cost more than a compact model.
For someone who only makes rings and earrings, that additional width may provide little practical benefit.
For a jeweler who expects their work to expand, however, it can reduce the chance of buying a smaller mill and replacing it later.
Choose around 130 mm if: sheet rolling is important to you, you make cuffs or larger pieces, or you would rather buy additional capacity once than upgrade because of width.
Not necessarily.
A large rolling mill is useful when you genuinely need its capacity. Bigger is not automatically better.
A 140–165 mm or wider mill starts to make more sense when:
For ordinary rings, earrings, bezels and pendants, much of that roller width may sit unused.
Larger mills also demand more from the workspace. Consider the mill itself, the handle sweep and the room needed to feed long strips of metal through both sides.
A compact workshop can benefit more from a correctly sized mill than from the widest mill it can technically accommodate.
A simple way to choose a size is to work backwards from your jewelry.
Ask: what is the widest single piece I reasonably expect to roll?
If the answer is 30 mm, buying a very wide flat mill solely for capacity is difficult to justify.
If you regularly want to roll 70–80 mm cuff blanks or texture a large sheet in one pass, a combination mill with only 50 mm of smooth area would be restrictive even if the manufacturer calls it a 110 mm mill.
Give yourself some spare capacity rather than choosing a roller that exactly matches your largest current piece.
That extra room helps with:
You do not need to double your required width, but buying with some margin above your normal work is sensible.
Suppose most of your work consists of:
Your sheet rarely exceeds 40–50 mm.
In this case, an approximately 75–100 mm combination mill may be perfectly adequate, provided its actual flat section accommodates your sheet.
Spending significantly more for a very wide mill may not improve the work you actually do.
Now consider a jeweler who wants to make:
Usable sheet width becomes much more important.
A nominally wide combination mill can still prove restrictive if much of the roll contains wire grooves.
This is a case where a 120–130 mm mill with a sufficiently wide flat area — or a dedicated flat mill — can make much more sense.
Beginners have a harder decision because they do not necessarily know what they will be making in two years.
If your budget permits it, a mid-sized 100–130 mm mill generally leaves more room to grow than the smallest mini mills.
That does not mean every beginner needs a professional 130 mm machine.
The better question is:
Am I buying a mill specifically for small components, or do I want this machine to become a long-term part of my bench?
For occasional hobby use and small projects, compact can be sensible.
For a mill you expect to keep while your metalsmithing expands, additional usable flat width and a good reduction gearbox are easier to appreciate later than they are on the day you buy it.
Width gets most of the attention because it is easy to understand, but it is not the only specification that affects what a mill can do.
Do not confuse roller width with roller diameter.
Width tells you how much lateral working space you have. Diameter describes the size of the cylindrical roller itself.
Roller diameter can affect the geometry and strength of the mill, the way it handles thicker stock and the overall size of the machine.
Two mills with the same 110 mm width can therefore still be substantially different tools.
For ordinary buying decisions, however, start with usable working width and then compare roller diameter between otherwise similar models.
The maximum opening tells you the thickest material the mill can accept.
This matters particularly if you plan to:
Do not assume a wider mill automatically has a larger opening. Width and opening are separate specifications.
Once you have enough capacity for your projects, gear reduction may matter more to day-to-day use than another 10 or 20 mm of width.
A reduction gearbox trades additional handle rotation for mechanical advantage, making heavy reductions easier to control.
This is especially useful when:
A narrow high-quality geared mill can be a better workshop tool than a wider mill that is unpleasant to operate. See rolling mill gear ratios explained for more on how gearing affects effort.
Choose the roller configuration around the work you actually do.
Combination mills are attractive as a first machine because one tool covers several operations. The cost of that versatility is reduced flat-sheet width.
Do not measure only the base of the machine. A rolling mill needs working clearance around it.
Allow room for:
A 130 mm mill may fit on the bench physically while still being awkward to use because the handle strikes a wall or another tool.
If you are planning a small workshop, include the mill when laying out your jewelry bench setup.
If you plan to use a rolling mill for textures, yes.
The relevant dimension is not necessarily the full width of the texture plate. It is the width of the piece of metal and texture material that must pass through the smooth section of the rollers.
Before choosing the mill, check the texture sizes you are likely to use.
This is another reason usable flat width deserves more attention than the headline roller dimension.
For normal jewelry work, you should choose a mill capable of accepting the useful width of the work rather than planning around repeated overlapping passes.
Trying to compensate for insufficient roller width by shifting wide sheet sideways can create inconsistent reduction and unwanted marks.
If wide sheet is going to be a recurring requirement, buy enough usable flat width for it.
For occasional oversized work, buying pre-rolled sheet can be more sensible than purchasing a much larger mill that otherwise sits underused.
Sometimes.
A rolling mill is the type of workshop equipment that can remain useful for many years, so buying slightly more capacity than you currently need can be rational.
But there is a difference between room to grow and buying unnecessary capacity.
A larger mill generally means:
If your foreseeable work fits comfortably within a 100–110 mm machine, there is no rule saying a 130–165 mm mill will make better jewelry.
Buy around the work, not around the largest number in the specifications.
This is the biggest mistake.
A 110 mm combination mill may offer much less than 110 mm of smooth sheet capacity.
Look for flat area, flat rolling width or the manufacturer’s roller diagram.
A project that only just fits leaves little margin for feeding and future work. Some spare capacity is useful.
Roll width does not tell you everything about frame stiffness, gears, bearings, roller hardness or build quality.
A wider low-cost mill is not automatically more capable than a narrower well-built one.
You interact with the gearing on every pass.
Once a mill is wide enough for your work, mechanical advantage can matter more than extra unused roller width.
Measure your workshop, not just the product dimensions.
A mill that cannot be operated comfortably in its intended position is effectively the wrong size.
It is easy to imagine needing huge sheets one day.
Look at what you actually make — and what you realistically plan to make — before paying for capacity.
A useful starting point is:
Most importantly, check the usable flat area rather than buying from nominal roller width alone.
For most home jewelers, the right mill is not the widest mill available. It is the smallest well-built mill that comfortably handles the widest work you expect to make, with enough spare capacity that you are unlikely to outgrow it immediately.
If you are ready to compare specific machines, see our guide to the best rolling mills for jewelry making.
For many beginners, approximately 100–110 mm is a useful middle ground because it provides more room to grow than a miniature mill without the size and expense of a large studio machine. A smaller 75–80 mm model can still be appropriate if you mainly make rings, earrings and other small pieces.
Yes. An 80 mm mill can handle a substantial amount of small jewelry work, particularly rings, bezel strip, earrings, wire and small pendants. It becomes restrictive when you start rolling wider sheet, larger texture plates or cuff blanks.
It can be if you regularly work with wider sheet, cuffs or larger textured pieces, or want additional capacity for future projects. If nearly everything you make is below 40–50 mm wide, much of the extra capacity may go unused.
Not always. On a flat rolling mill they can be similar, but a combination mill uses part of its roller for wire grooves. A mill advertised as 110 mm wide may therefore have a substantially narrower smooth flat section.
Roller width measures the working length across the face of the roller and affects how wide a piece can be rolled. Roller diameter measures the size of the roller from one side of the circle to the other. They describe different aspects of the mill.
Choose a flat mill if sheet reduction and texture work dominate what you do. Choose a combination mill if you want both sheet rolling and wire grooves in one machine. Remember that the wire grooves reduce the smooth flat area available on a combination mill.
Yes, but check the usable flat width against the width of the cuff blank you intend to roll. A larger 120–130 mm-class mill or a flat mill may be preferable if wide cuff work is a regular part of your jewelry making.
It needs enough smooth working area for the metal and texture setup you intend to pass through it. Check the actual flat rolling width rather than assuming the mill's total advertised roller width is available for texture work.
We have not personally used every product in this guide. Recommendations are based on specifications, manufacturer documentation, specialist references and owner experiences.
Full details: how we review and research tools and oureditorial policy.
Buying guide · Rolling & Forming
Choose the right jewelry rolling mill by roller width, configuration, gearing and bench space, with a research-based look at budget and professional options.
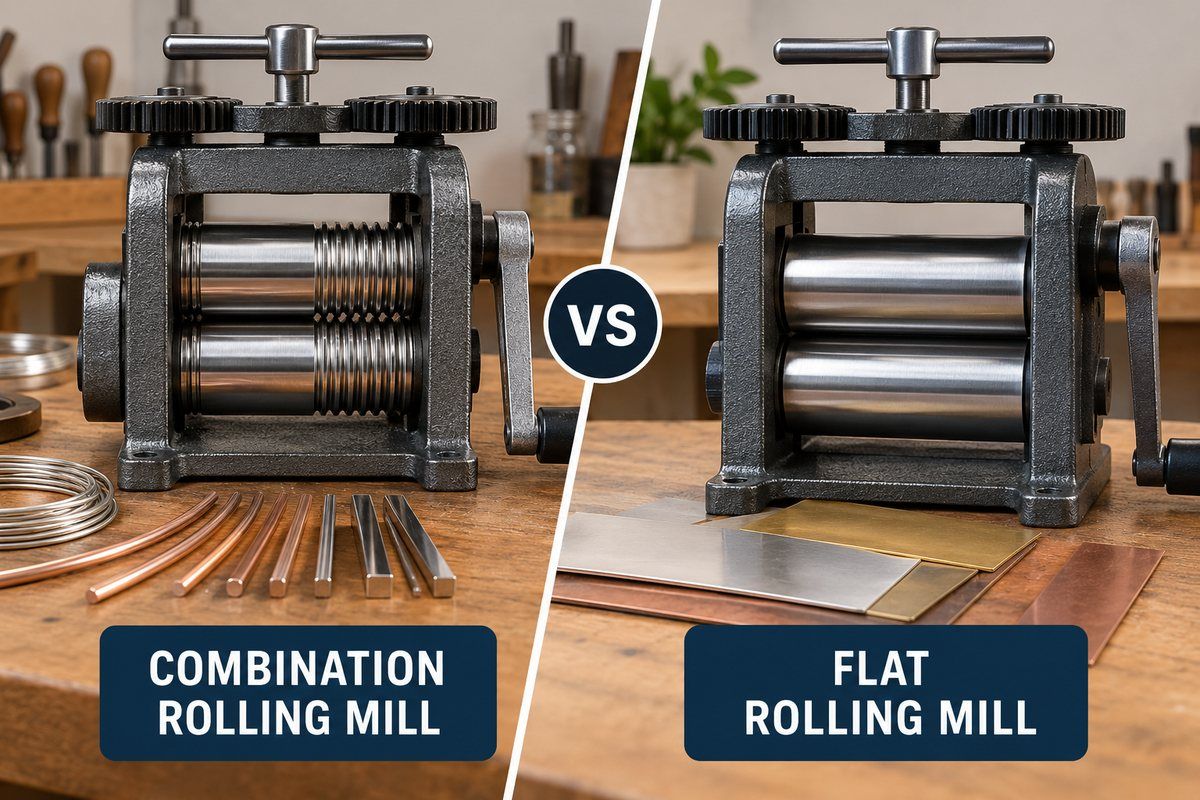
Comparison · Rolling & Forming
Combination vs flat rolling mills compared for jewelry making — including usable sheet width, wire grooves, versatility and which type is better for your bench.
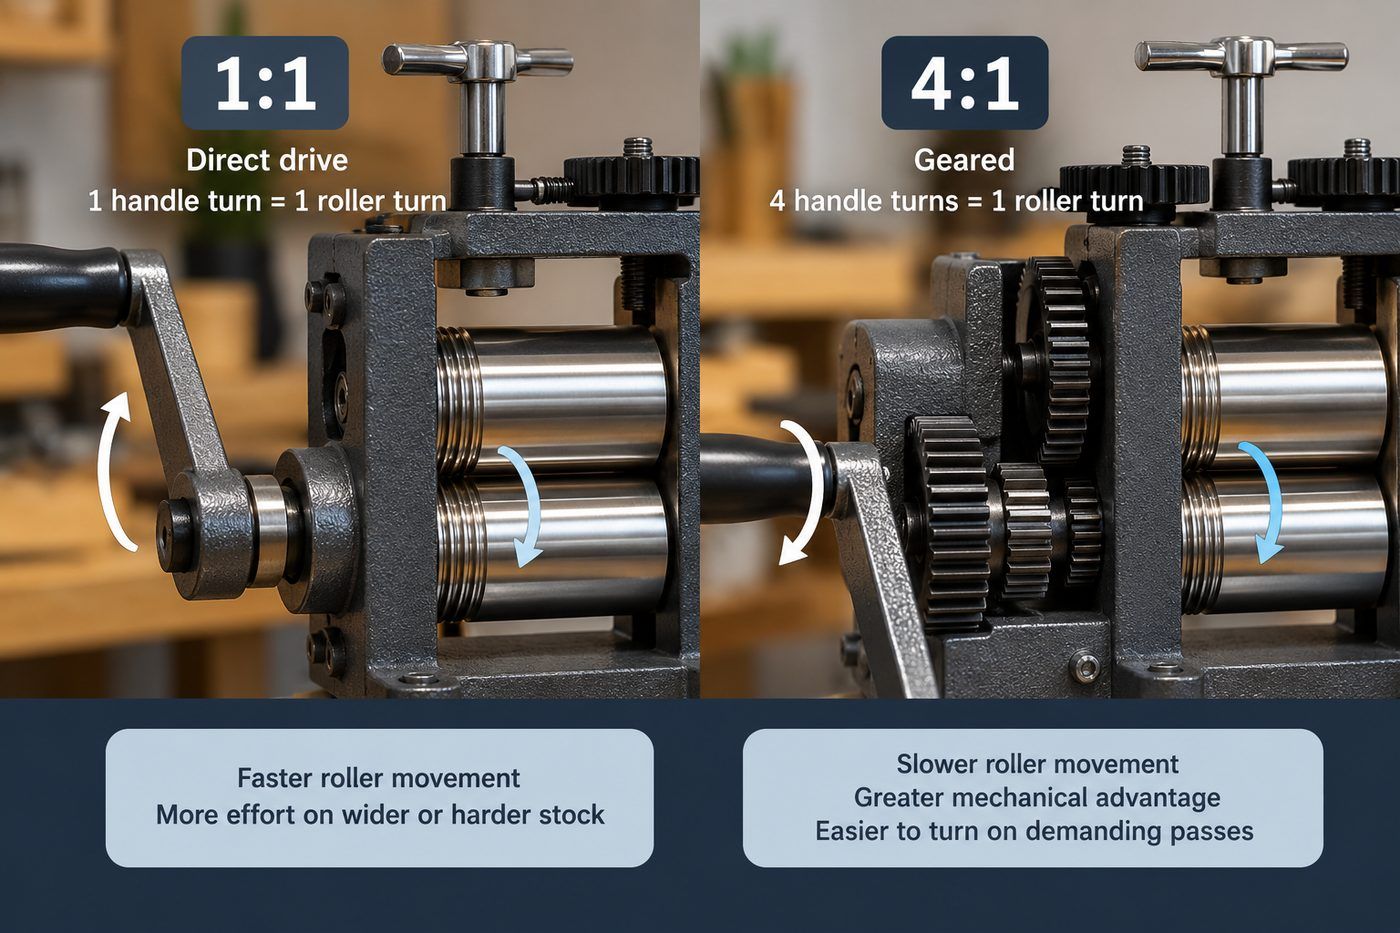
Explainer · Rolling & Forming
Learn what 1:1, 2:1 and 4:1 rolling mill gear ratios mean, how reduction gearing changes torque and handle effort, and whether a geared rolling mill is worth it.
Comparison · Rolling & Forming
Compare VEVOR and Durston rolling mills on gearing, roller finish, alignment, usable width, durability and support to decide whether a premium mill is worth the extra cost.